Strategic Guidance. Sustainable Solutions. Measurable Impact.
Hitech Green Energy Consultants
38+ Years of Chemical Engg. & Founder Leadership

Engineering Leadership inTyre Pyrolysis & rCB

Er. V.K. Srivastava is the Founder & CEO of Hitech Green Energy Consultants (est. February 2026). With a Chemical Engineering (HBTI) and MBA background, he serves as Senior Advisor to top management across India and global markets—specializing in continuous tyre pyrolysis, recovered carbon black (rCB) enhancement, and mechanical tyre recycling solutions.

1987Career Started
38+Founder Experience
92-95%Audit Scores
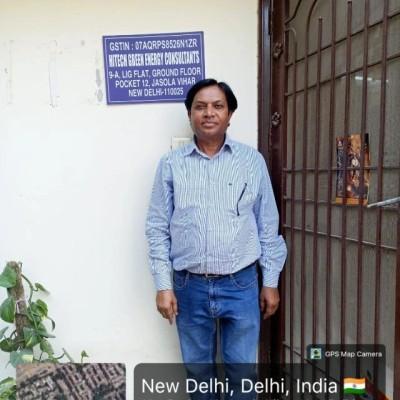
Er. V.K. Srivastava - Founder & CEO of Hitech Green Energy Consultants, Industrial Recycling & Tyre Pyrolysis Expert

Er. V.K. Srivastava

Founder & CEO

HBTI B.Tech (Chem Engg.) 1987MIBM MBA (Operations) 2017B.Sc University Top Rank HolderAIRTRA Expert Consultant
Technical Competence

Core Consulting Domains

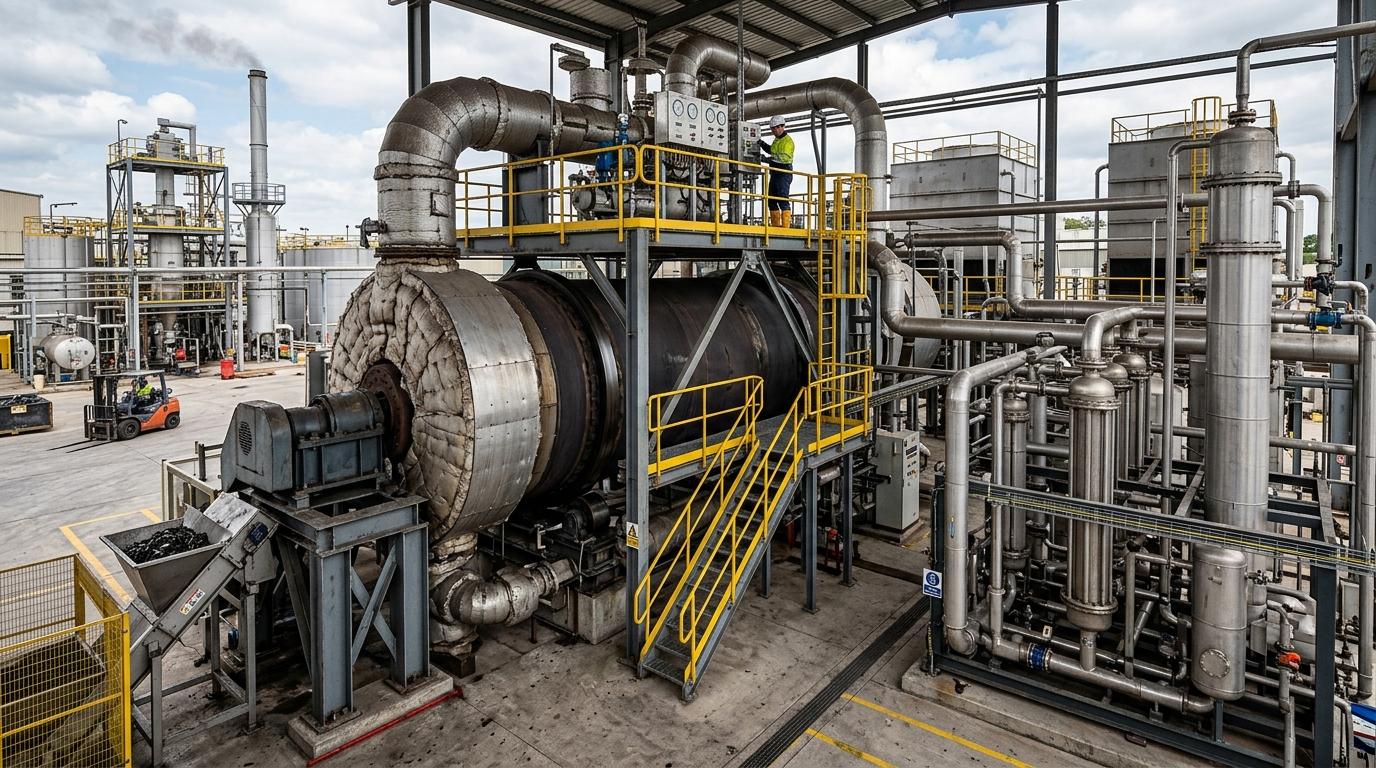
Commercial rotary tyre pyrolysis reactor with vapor condensation system
01

Continuous Tyre Pyrolysis

Specialized engineering advisory with major focus on industrial-scale continuous pyrolysis operations, automated feeding & discharge, and DCS/SCADA process optimization.

  • Continuous Pyrolysis Operations (Primary Focus)
  • Automated Continuous Feeding & Char Discharge
  • PLC, SCADA & DCS Continuous Process Controls
  • Semi-Continuous & ABAP Systems Benchmarking
Explore Scope
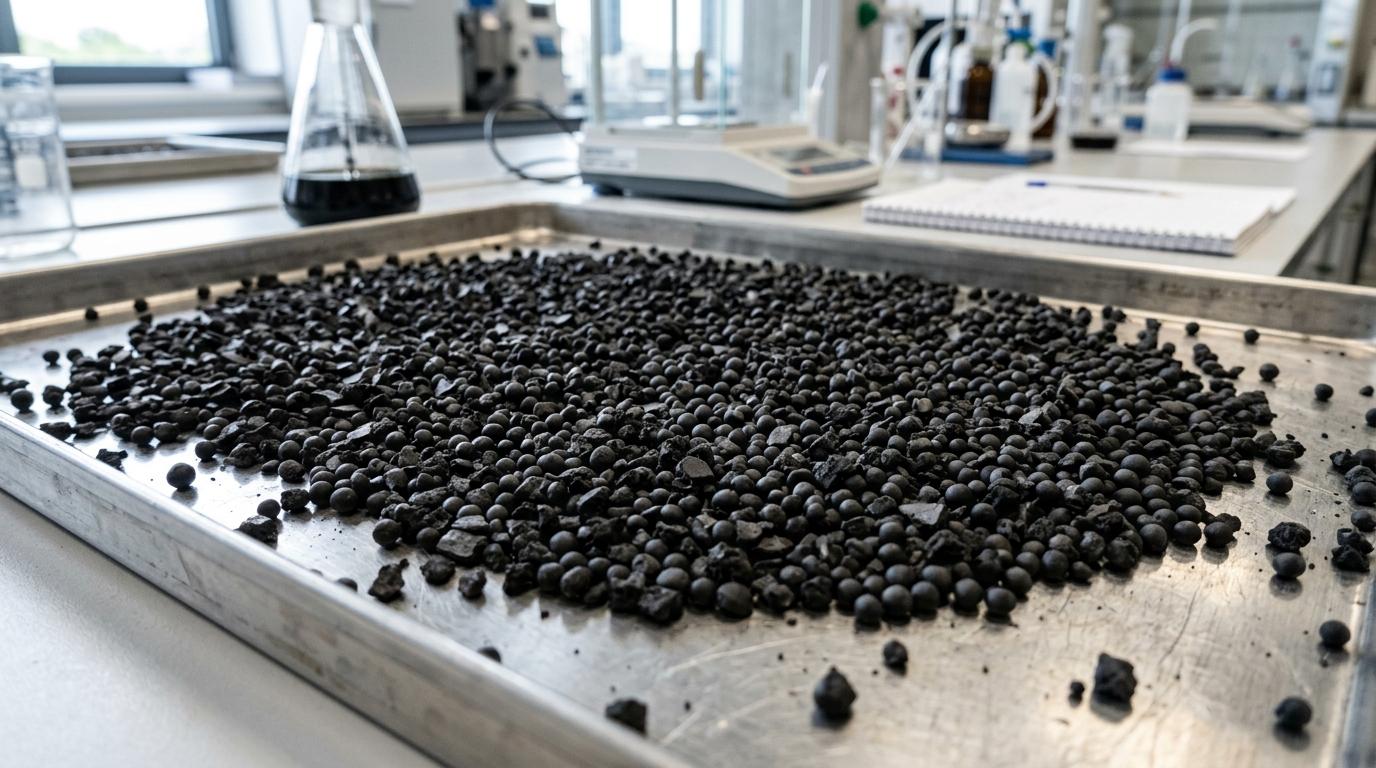
High-purity recovered carbon black (rCB) micro-pellets post-purification
02

rCB Enhancement

Improving the quality and value of recovered carbon black to international standards.

  • Physical Purification
  • Grinding & Jet Milling
  • Pelletization Process
  • Technical Drying Systems
Explore Scope
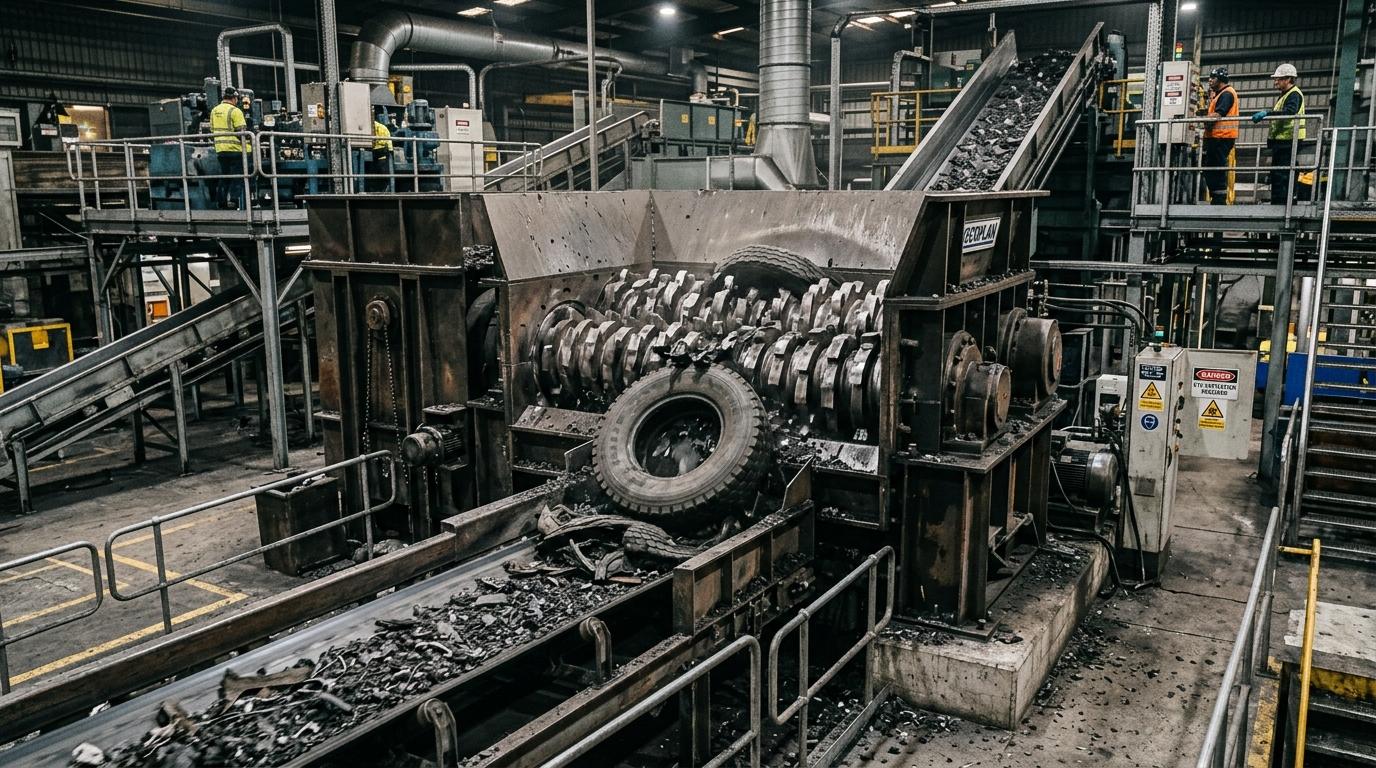
Heavy-duty industrial dual-shaft tyre shredder sizing tyre scrap
03

Tyre Recycling

Mechanical size-reduction and material separation systems for tyre feedstock.

  • Tyre Shredding Solutions
  • Rubber Chips (Mulch) Production
  • Crumb Rubber Granules and Powder Production
Explore Scope
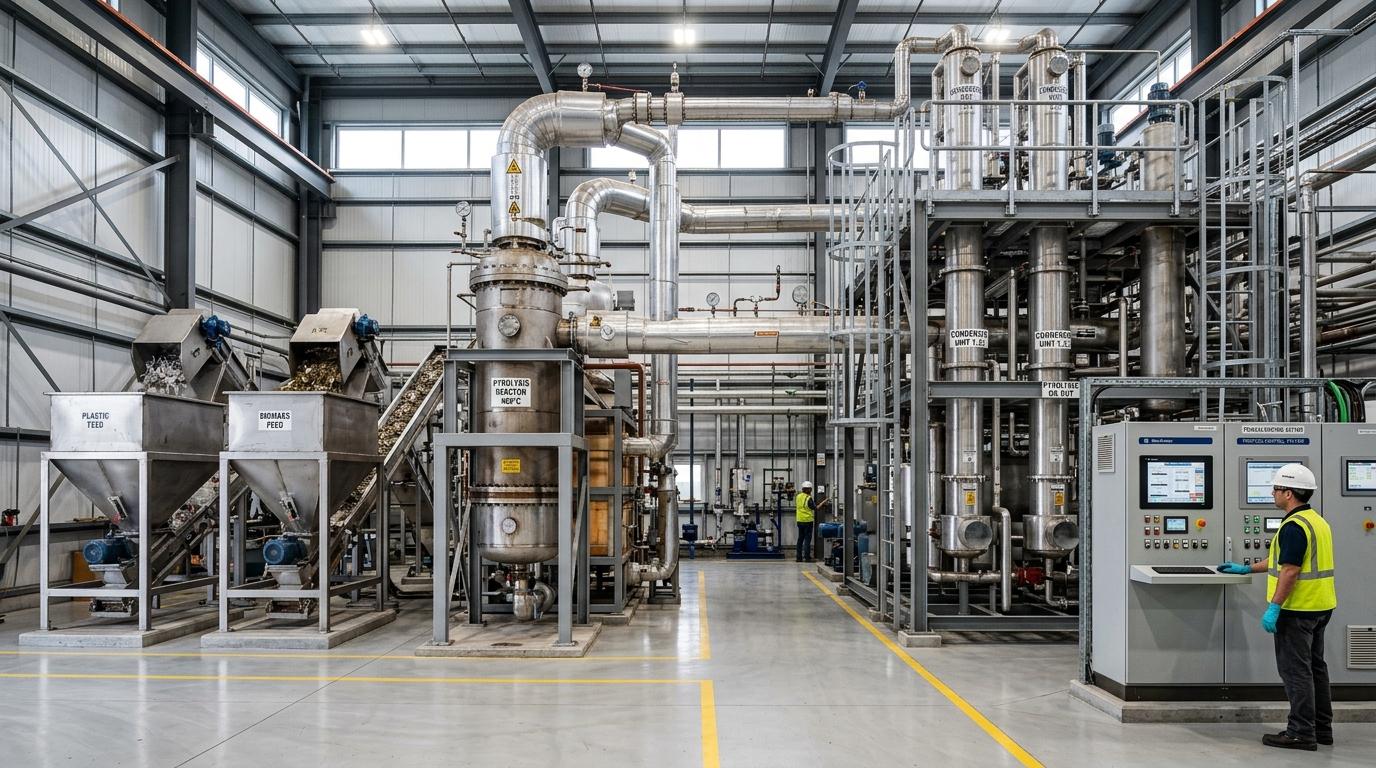
Continuous industrial plastic and biomass thermochemical pyrolysis conversion plant
04

Plastic & Biomass Pyrolysis

Technology assessment and chemical processing setup for alternative feedstocks.

  • Plastic Waste Pyrolysis
  • Biomass Thermochemical Conversion
  • Feedstock Evaluation
Explore Scope
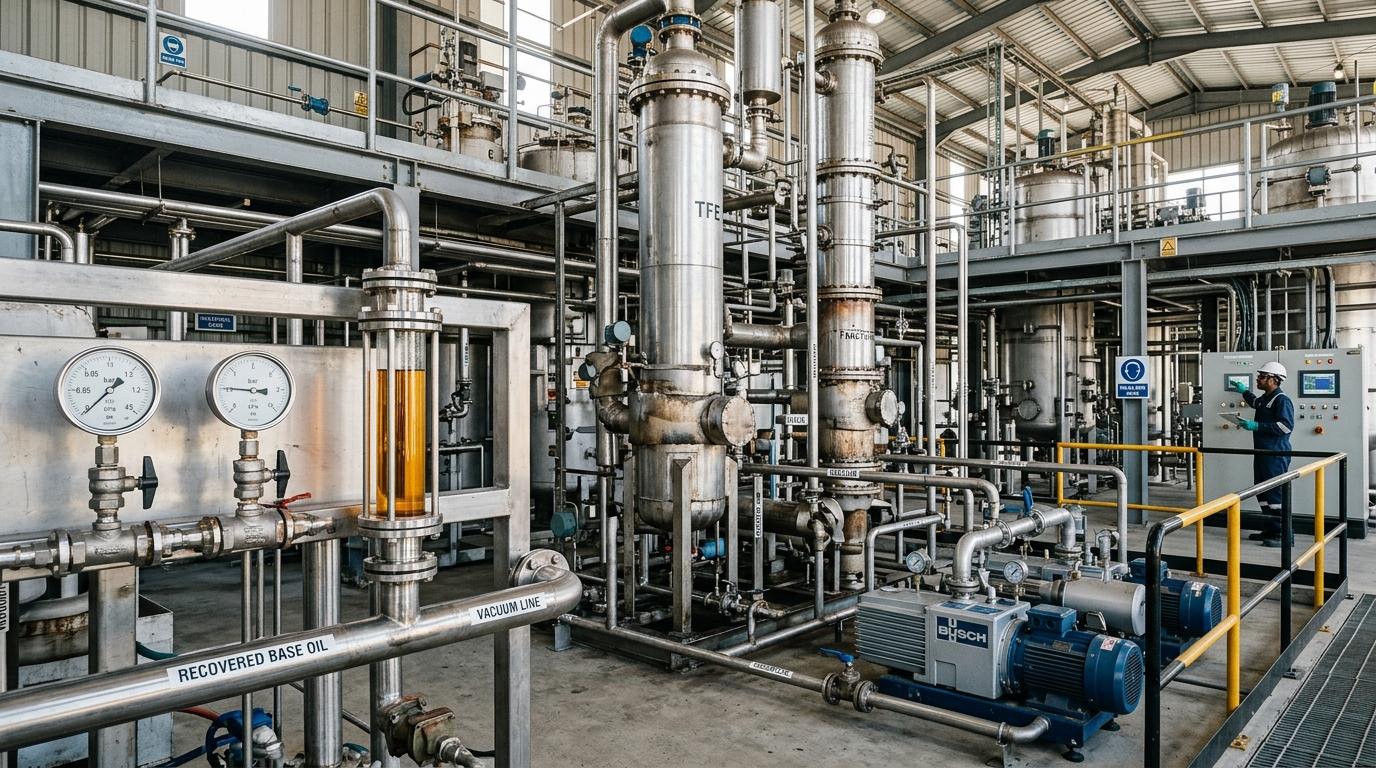
High-vacuum thin-film evaporator (TFE) base oil recovery unit
05

Base Oil Recovery

Refinery and recycling consultation for industrial lubricant and base oil reclamation.

  • Base Oil Recovery Processes
  • Quality Compliance Advisory
  • Value-added Product Optimization
Explore Scope
Core Strengths

Professional Capabilities

Strategy & Business

  • Strategy Consulting
  • Strategy
  • Business Strategy

Manufacturing & Operations

  • Manufacturing
  • Manufacturing Operations
  • Manufacturing Operations Management

Process & Continuous Improvement

  • Process Optimization
  • Process Improvement
  • Continuous Improvement

Technical & Industrial

  • Chemical Engineering
  • Chemistry
  • Plastics

Leadership & Commercial Operations

  • Leadership
  • Team Management
  • Team Building
Core Technical Bench Strength

Core Technical Team

Multi-Disciplinary Engineering & Science Support:Highly qualified professionals with Ph.D in Chemical Engg. / Organic Chemistry, M.Tech & B.Tech in Chemical & Petrochemical Engg., and M.Sc in Organic Chemistry are part of our core technical team — as a support to the organisation for the value additions.

Doctoral Research
Ph.D

Chemical Engg. & Organic Chemistry

Reaction Kinetics & Molecular Thermodynamics

  • Advanced pyrolysis cracking mechanics and reaction pathways
  • Catalytic synthesis and thermal decomposition kinetics
  • Deep thermodynamic modeling for high-yield product recovery
Core Advisory Bench
Scale-Up & Engineering
M.Tech & B.Tech

Chemical & Petrochemical Engg.

Industrial Continuous Plants & DCS/SCADA Systems

  • Continuous reactor scale-up, mass and energy balance design
  • DCS, PLC & SCADA industrial automated process integration
  • Refinery-grade condensations, safety HAZOP, and EHS protocols
Core Advisory Bench
Material Science
M.Sc

Organic Chemistry

Hydrocarbon Analysis & Surface Chemistry

  • Recovered Carbon Black (rCB) surface activation and de-ashing
  • Volatiles reduction, pelletization, and jet-milling optimization
  • Polymer matrix compatibility and masterbatch test alignment
Core Advisory Bench
Operational Support
Strategic Focus

Value Additions to Client Organizations

Plant Floor to Boardroom Advisory Support

  • Independent technology, reactor, and vendor vetting
  • Process bottleneck diagnosis and OPEX/CAPEX optimization
  • Commissioning assistance and customer audit quality readiness
Core Advisory Bench

Value Addition Mission: Delivering rigorous chemical kinetics, continuous plant scale-up, and analytical carbon black science as active advisory support for industrial clients worldwide.

Our Differentiator

From Plant Floor to Boardroom

Bridging Engineering Excellence with Business Leadership

Career Evolution Journey

“Technical depth. Operational experience. Executive judgment.”

1
Technical DepthChemical Engineer
2
Technical DepthProcess Engineer
3
Operational DepthProduction / Manufacturing Leader
4
Operational DepthPlant / Factory Head
5
LeadershipOperations Leader
6
Business JudgmentProfit Center / Business Head
7
Executive AdvisorySenior Advisor
8
Strategic VisionFounder & CEO

Plant Floor

Industrial consulting that understands physical realities. We advise on production scheduling, process safety parameters, machinery layouts, and EHS requirements directly on the floor.

Process & production execution
Machinery & equipment setup
Quality control & assurance
EHS compliance & safety management
Shop-floor & labor relations
Process controls (PLC/SCADA/DCS)

Boardroom

Executive-level guidance mapping engineering to finance. We assist with technology vendor assessments, CAPEX calculations, profitability strategies, and preparing for critical client and stakeholder audits.

Techno-commercial strategy
CAPEX & project cost optimization
P&L tracking & profitability improvement
Technology & vendor assessment
Customer audit facing (92-95% scores)
Organizational policy & scaling decisions
Proven Operational & Yield BreakthroughsPAN India & Global Markets

Key Achievements in Tyre Pyrolysis & rCB Enhancement

Direct engineering and operational impact delivered on plant floors—optimizing yields, eliminating product defects, extending continuous reactor cycle times, and establishing commercial off-take.

01
+5% Net Yield Gain
Oil Yield Improvement
40–41% → 43–46%

Elevated Tyre Pyrolysis Oil (TPO) Yield

Improved the Tyre Pyrolysis Oil (TPO) yield from 40–41% to 43–46% for both the same and varying feedstocks, achieved by virtue of thermochemical process optimization, refined temperature zoning, and executing strict operational controls.

Verified Operational Impact
02
Loss Elimination
Condensation Efficiency
Maximized

Enhanced Liquid TPO Recovery

Enhanced net liquid oil recovery and condensation throughput across multi-stage condenser loops, minimizing volatile losses and syngas carryover to capture maximum saleable liquid fuel per metric ton processed.

Verified Operational Impact
03
Consistent Commercial Grade
Specific Gravity (Density)
0.92–0.93 → 0.90–0.91

Refined Oil Density & Specific Gravity

Consistently improved the Oil Density (Specific Gravity) from 0.92–0.93 down to 0.90–0.91 by changing critical process parameters—eliminating heavy sediment and making the oil reliably saleable at premium industrial rates.

Verified Operational Impact
04
Conquered #1 Industry Bottleneck
Continuous Uninterrupted Run
20 → 50+ DaysBreakthrough

Competitor/Standard Plants run only 25–35 days max

Extended Continuous Plant Production Cycles

Enhanced the running days of production cycles in Continuous Tyre Pyrolysis Plants from 20 to 50+ days while maintaining peak TPO yield and product quality. This solves the biggest challenge in Continuous Pyrolysis (majorly in Rotary-type Continuous Reactors and Screw-type Reactors), where standard plants run for only 25–35 days max.

Verified Operational Impact
05
Full Commercial Support
Purified rCB & Market Off-take
High-Grade

Enhanced rCB Quality & Strategic Sales Promotion

Enhanced the overall physical and chemical quality of Recovered Carbon Black (rCB) through post-pyrolysis purification and ash management, accompanied by fullest strategic support in sales promotion and buyer qualification for client companies.

Verified Operational Impact
Industry Proven

Leadership at India's Top Tyre Recycling Plants

“Having served India's top-ranked companies in the tyre recycling business at the highest operational capacity at the plant level, this hands-on mastery provides the strong base, technical strengths, and unshakeable confidence required while undertaking the role of Consultant / Advisor for tyre recycling solutions across PAN India and globally.”

Consulting Scope

How We Help Organizations Grow

01

Technical Advisory

Rigorous technical reviews, technology selection guidance, and chemical engineering process optimization.

Technology evaluationPlant/process assessmentTyre pyrolysis advisoryrCB enhancement advisory
Learn More Services
02

Projects & Operations

Hands-on execution oversight, commissioning advisory, vendor sourcing, and machinery evaluation for industrial recycling plants.

Project management supportMachinery evaluationVendor assessmentPlant operations advisory
Learn More Services
03

Management & Boardroom Advisory

High-level techno-commercial strategy, P&L improvement programs, customer audit preparation, and executive mentoring.

Techno-commercial advisoryP&L-oriented decision supportBusiness growth strategiesOrganizational improvement
Learn More Services
Process Lifecycle

Our Solution Flow — Tyre to Value

01

Scrap Tyres

Incoming feedstock source

02

Tyre Shredding

Mechanical processing and sizing

03

Continuous Pyrolysis

Continuous automated thermal cracking & condensation

04

Recovered Products

Separation into Oil, Steel, and Raw Char

05

Raw Char

Pre-enhancement input material

06

rCB Enhancement

Physical purification stages

07

Purification

Removal of ash and inorganic residues

08

Grinding

Particle size reduction

09

Pelletization

Micro-pellet compounding

10

Drying

Moisture removal

11

Enhanced rCB

High-value commercial output

WHY TYRE RECYCLING MATTERS

Why Tyre Recycling Matters

Turning end-of-life tyres into valuable resources — while supporting resource efficiency, responsible waste management and a more circular industrial economy.

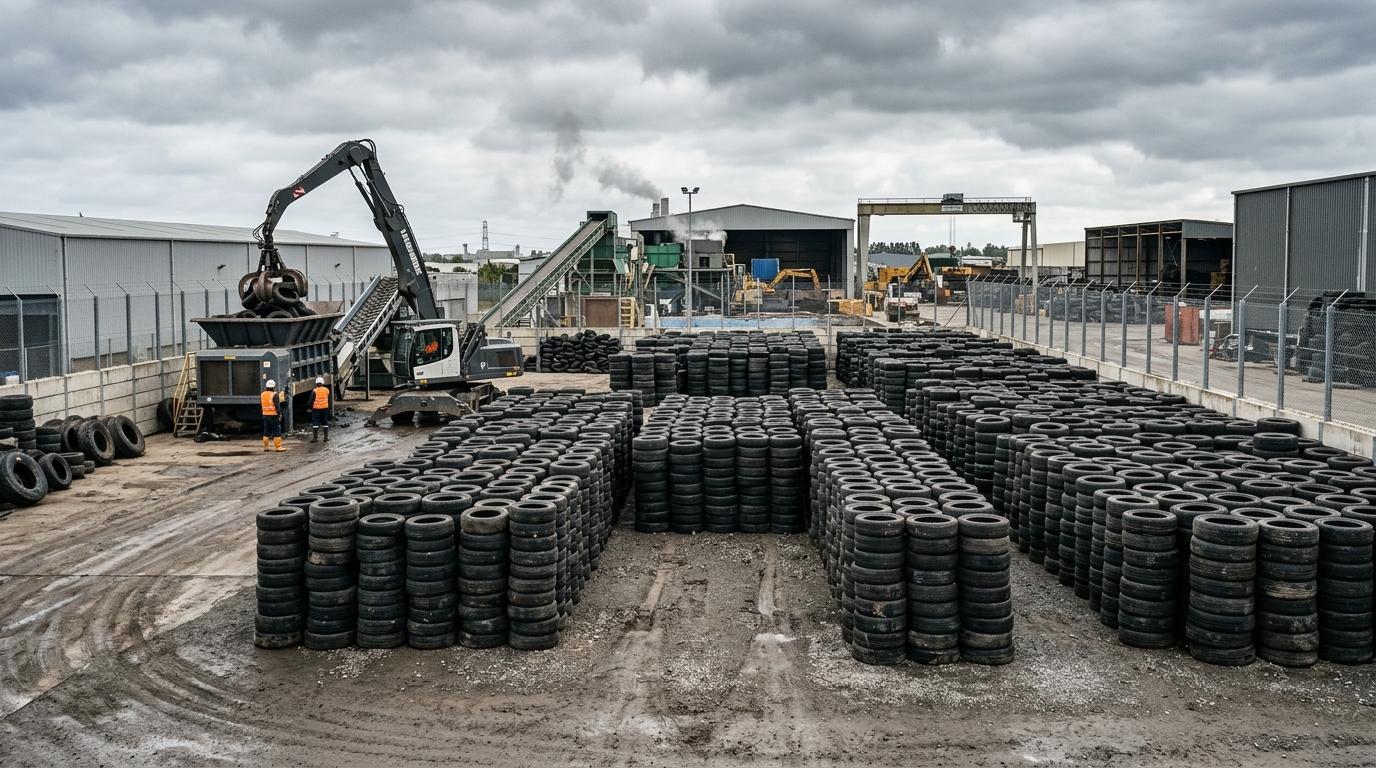
Organized industrial scrap tyre collection and storage yard at a material recovery facility
Feedstock Logistics & StorageMaterial Recovery Facility
Industrial Feedstock Transformation

Transforming Industrial Waste Liabilities into Secondary Feedstocks

End-of-life tyres represent one of the most durable, energy-dense rubber waste streams in the global industrial economy. When managed through engineered mechanical shredding, devulcanization, or thermochemical pyrolysis, these scrap tyres cease to be environmental liabilities and are systematically recovered as valuable secondary raw materials.

Virgin Resource Displacement
Controlled Environmental Safety
Closed-Loop Value Cycles
01
Virgin Feedstock Substitution

Resource Recovery

Responsible tyre recycling enables the recovery of polymer rubber, hydrocarbon oils, and high-tensile steel wire from end-of-life tyres, helping reduce industrial reliance on virgin fossil feedstocks.

Scope note: Material recovery efficiency and grade suitability depend on feedstock classification, tyre sizing, and plant separation technology.

02
Resource-Efficient Secondary Inputs

Energy & Carbon Efficiency

Processing secondary rubber fractions and recovered carbon black (rCB) generally requires lower thermal and electrical energy than synthesizing virgin petroleum polymers and furnace carbon black.

Scope note: Net energy balances vary based on reactor design, condensation efficiency, and process heat recirculation systems.

03
Controlled Processing vs. Unmanaged Stockpiles

Responsible Waste Management

Engineered tyre recycling provides an environmentally controlled alternative to unmonitored disposal, helping mitigate the fire hazards and uncontrolled environmental footprint associated with scrap tyre accumulation.

Scope note: Environmental performance is contingent on robust plant-level EHS protocols, gas scrubbing, and process safety engineering.

04
Closed-Loop Secondary Industrial Applications

Circular Material Value

Depending on the processing route—whether mechanical shredding or thermochemical pyrolysis—derived outputs can be reintroduced into commercial masterbatches, molded rubber goods, and industrial fuels.

Scope note: Output product yields, mesh sizes, and commercial purity grades require project-specific technical assessment and founder verification.

Evaluating a tyre recycling, pyrolysis, or rCB enhancement initiative?

We provide independent techno-commercial assessments, machinery evaluation, and operational advisory.

Discuss a Circular Economy Project
Professional Journey & Credentials

Professional Journey & Leadership Background

Founder & CEO, Hitech Green Energy Consultants — Advisory in Tyre Recycling Solutions

View Full Journey & Achievements

LEADERSHIP EXPERIENCE

  • 1.Operations & Projects Head
  • 2.Manufacturing Head
  • 3.Unit Head
  • 4.Profit Center Head
  • 5.Business Head (Techno-Commercial)
  • 6.Site Head/Director-Operations (Whole Time Director/Occupier)
Whole Time Director to Founder & CEO

TECHNICAL EXPERTISE

  • 1.Continuous Tyre Pyrolysis (both Rotary & Screw type), Semi-continuous Tyre Pyrolysis & ABAP (Advance Batch Automated Process)- with exposure to Indigenous & abroad technologies
  • 2.SCADA/DCS/PLC/HMI controlled Plant operations
  • 3.5S/Kaizen/TQM/TPM/IATF systems
Continuous, Semi-Continuous & ABAP

INTERNATIONAL EXPOSURE

  • 1.Indian Toners & Developers Ltd. (Technical collaboration with Elfotech AG Switzerland)
  • 2.Rathi Graphic Technologies Ltd. (Technical collaboration with Raven Industries Inc. USA)
  • 3.Continental Carbon India Ltd. (MNC)
Switzerland, USA & Global MNCs

ACHIEVEMENTS & AUDITS

92–95%Customer Audit Scores

Audited & approved by MRF, J.K. Tyres, Apollo, BKT, Continental, CEAT, Goodyear & Pfizer Inc.

Excellent Category Rating
Interested in Plant-Level Track Records & Verified Turnkey Results?Review verified operational achievements across Acmechem, Rathi Rubber, Royal Carbon & Continental Carbon.
Explore Plant Achievements
Sectors Covered

Industries We Serve

Professional techno-commercial and operations advisory tailored for primary recycling segments and broader chemical sectors.

Primary Industrial Specialization

Tyre Recycling

Core Advisory Domain

Pyrolysis Plants

Core Advisory Domain

Recovered Carbon Black (rCB)

Core Advisory Domain

Industrial Chemicals

Core Advisory Domain
Broader Industry Sectors Served
Chemical Manufacturing
Petrochemicals
Rubber Chemicals
Carbon Black
Specialty Chemicals
Agrochemicals
Pharmaceuticals / APIs
Paints & Resins
Masterbatches
Toners
Knowledge Center

Technical Insights & Guidance

Explore Knowledge Center
Industry Endorsements

Professional Recommendations

01/10• Swipe or click dots to browse
Technology & Leadership

“I know Mr. Veerendra for the last 10 years. He has following distinct natural qualities : 1. Good Understanding of technology and it’s effect on environment and people. 2. Commercial evaluation of projects. 3. Self motivated. Inspiration other people too. 4. Hard task master and follow up till the desirable results are achieved. 5. Takes the team into confidence by clear communication. 6. He remains deeply involved in his work . 7. His mind remains stable and peaceful and balanced at the time of crisis 8. He is honest, hardworking. 9. Reliable and trustworthy.”

TP

Tej Prakash Srivastava

Global Fertilizer Advisor – Technical Excellence & Sustainable Growth

Tej Prakash was senior to Er. V.K. but didn't manage Er. V.K. directly

Focus & Results

“Veerendra Kumar Srivastav ji is a hard working , trust worthy and result oriented dynamic person.”

BK

Bijendra Kumar Pandey

Senior Management Professional (Plastics & Polymers Industries)

Studied together with Er. V.K.

Professional Reliability

“Mr. Srivastava is one of the sharpest minds I've met in our business industries. He has focused, clear in his objectives, strong capability to give a helicopter view and at the same time pay attention to the details. Mr. Srivastava is a passionate person who always does his job exceeded people expectation. He set example in self-discipline, hard work and endurance; striving to be the best in each assignment. If you are looking for service and reliability as professional you can count on him. There is a feeling of warmness talking to you every time you meet him, doesn’t matter which company-place be. I personally took many important lessons which are relevant in my career time in Paint Industries as he is very nice person by heart. Thank you very much Sir for giving me valuable support. I wish him good luck...”

SP

Sandeep P. Bahukhandi

CEO @ United Multichem | 20+ years experience | Aroma Chemicals & Essential Oils

Er. V.K. was Sandeep P.’s client

Commitment & Transparency

“I am please to share some of the great talents which I have learnt about Mr. Veerendra Kumar Srivastava. He is a man of commitment, well focus and a person who is expert in time management !! He is vocal, transparent, responsive and honest in his interaction which is a great asset for a person in senior management position. I always enjoy each and every interection be it personal or professional.”

AJ

Anil Jha

Founder Director @ AEON MARKET RESEARCH | Marketing Research, Analytical Skills

Er. V.K. was Anil’s client

Executive Results & Integrity

“Mr. Veerendra Kumar Srivastava is very industrious, honest, transparent and result-oriented Senior Management Executive.”

PK

Praveen Kumar Verma

Proprietor at M/s Indian Scientific Enterprises

Er. V.K. was Praveen Kumar’s client

Plant Turnaround & Competence

“Mr. VK srivastava comes across as a very hardworking colleague with excellent man management skills. He is an absolute Team player and can change the most ill managed setups with his enthusiasm and technical competence. With his vast experience across various sectors , he would be a valuable asset to any organization.”

AD

Amit Dikshit

Marketing professional

Worked with Er. V.K. on the same team

Technical & Administrative Soundness

“Mr. Veerendra Kumar Srivastava is very interactive, cooperative, unbiased, honest, practical , sincere & dynamic, intelligent and administratively / technically sound. He is very humble, disciplined, civilized and has great affection and regards for everybody (juniors, peers & seniors). I wish him all the best & great success in his future endeavors.”

DP

Dr. P. B. Jana

Consultant Rubber Technologist in Non-Tyre Rubber Sectors

Worked with Er. V.K. on the same team

Team Building & Transformation

“Veerendra Jee is one of the true professional who carry an excellent ability of being Polite, Humorous and Task Master with his team to bring best out of them. He happened to be a real Leader fighting from front to create a winning team..”

SR

Sandeep Rai

Co-Founder @ Ample Leap | Ex-CHRO & HR Leader | Leadership Hiring | HR Strategy | Business Transformation

Worked with Er. V.K. on the same team

Target Delivery & Strategic Vision

“Veerendra Sir is champion in his area, keeps his team highly motivated and his ability to get the best results by his team makes him champion. A number of times, he achieved tough targets very easily. His technical qualification and rich industrial experience makes him a perfect leader with clear vision. I wish him all the best in his future endeavors.”

SK

Sanjay Kr. Srivastava

Deputy General Manager-Operations at Birlanu Limited (Formerly HIL Limited)

Er. V.K. was senior to Sanjay Kr. but didn’t manage Sanjay Kr. directly

Leadership & Communication

“He is very hardworking, intelligent, good orator as well as communicator and very good leader.”

VV

Virendra Vikram Chaturvedi

Chief General Manager Incharge, Iron at Steel Authority of India Limited/ Durgapur Steel Plant

Studied together with Er. V.K.

Consultation Inquiry

Have an Industrial Challenge?

We specialize in evaluating new technology setups, optimizing existing plant processes, and analyzing the commercial viability of tyre pyrolysis and circular recycling initiatives. Let's explore how we can support your project.

New Delhi (Remote or In-Person)PAN India & Global Markets