Technical Expertise
Hitech Green Energy Consultants delivers senior-level engineering advisory for industrial recycling, pyrolysis, and chemical recovery. We guide projects from the plant floor to executive clearance.
Continuous Tyre Pyrolysis
Continuous thermochemical conversion of shredded scrap tyres into high-value pyrolysis fuel oil (TPO), steel wire, and recovered carbon black (rCB) char under fully automated continuous reactor environments.
Deep industrial specialization in continuous tyre pyrolysis systems, automated air-lock continuous feeding, temperature gradient control, syngas recirculation, and continuous char cooling. Proven leadership across continuous plants, semi-continuous facilities, and advanced automated batch (ABAP) operations.
Continuous plant engineering due diligence, continuous rotary reactor and furnace evaluation, air-lock feed & hot char discharge system design, automated DCS/SCADA closed-loop controls, process parameter standardization, mass and heat balance modeling, EHS risk mitigation, and continuous plant debottlenecking.
- Continuous Automated Pyrolysis Plants (Major Focus)
- Continuous Rotary Reactors & Multi-Zone Heating Controls
- Automated Air-Lock Feeders & Hot Char Discharge Systems
- DCS, SCADA & PLC Integrated Instrumentation
- Continuous Syngas Scrubbing & Fuel Recirculation Loops
- Semi-Continuous & Advanced Batch (ABAP) Comparative Audits
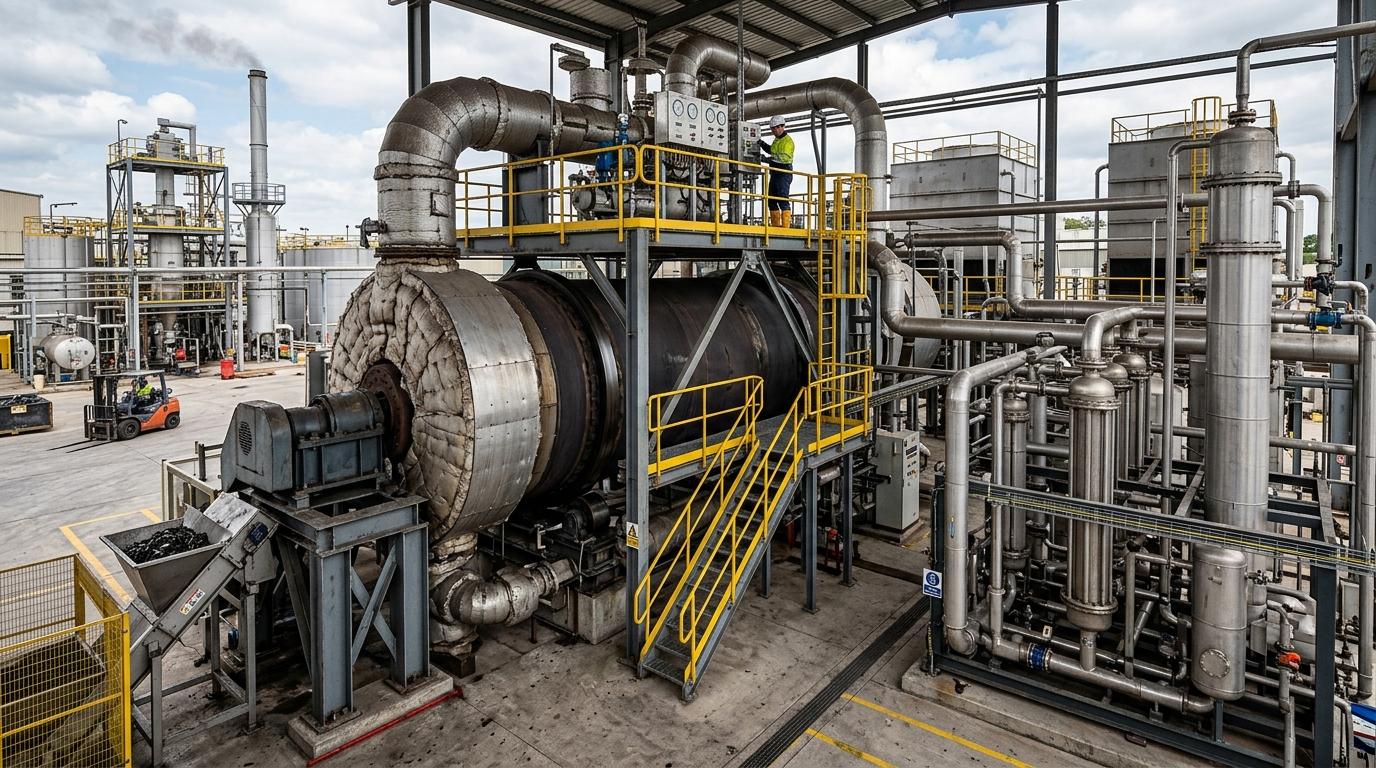
Continuous Thermochemical Conversion: Commercial continuous rotary pyrolysis reactor and condensation train
rCB Enhancement
Upgrading raw pyrolysis char through physical purification, grinding, and post-treatment to meet international grade Recovered Carbon Black (rCB) standards.
Led operations at Speciality Engineered Carbon Black divisions (e.g. Continental Carbon, Royal Carbon, and Finster Carbon). Collaborated with senior professors at IIT Delhi and IIT Hyderabad on technical enhancements.
Purification process design, grinding/jet milling technology selection, pelletization system advisory, and international-grade specifications matching.
- Physical Purification
- Grinding & Jet Milling
- Pelletization & Compounding
- Technical Drying Systems
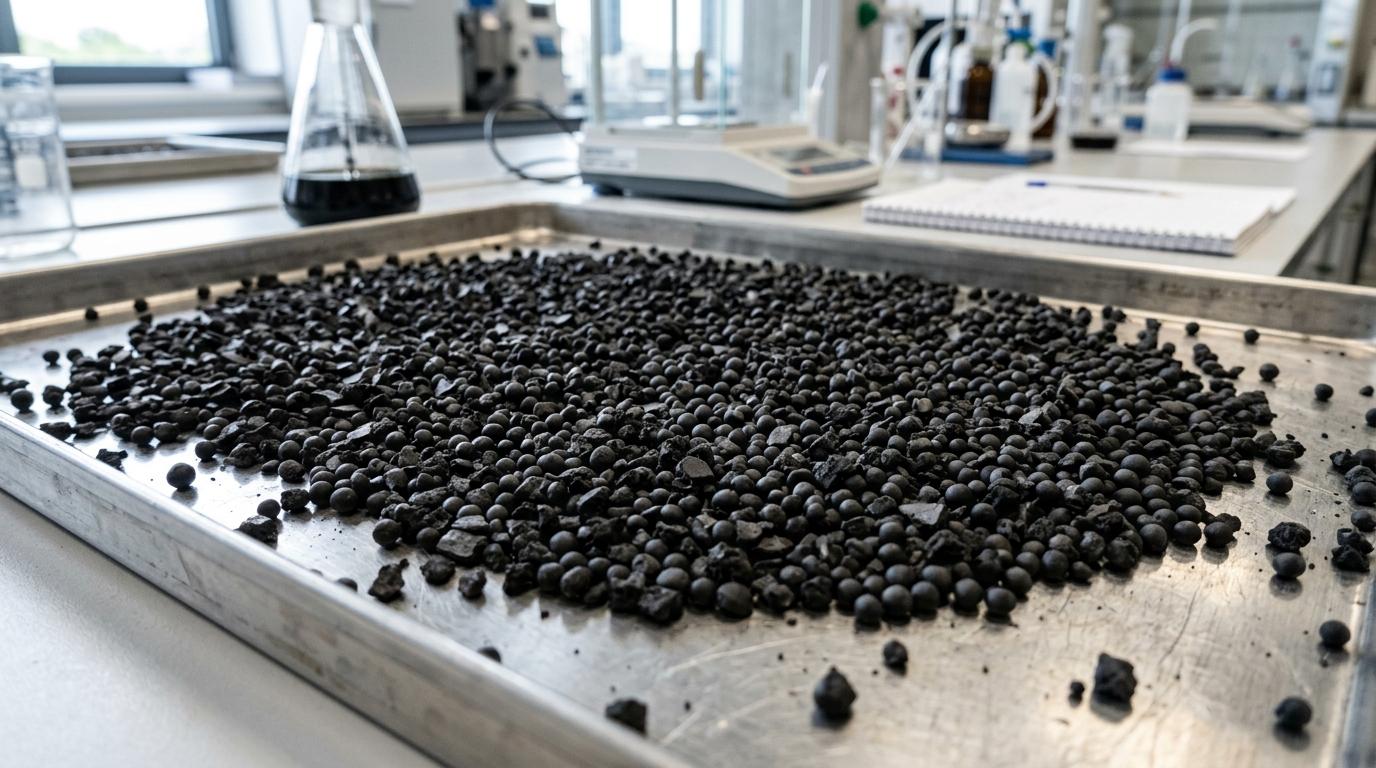
Technical Output: High-purity rCB micro-pellets post-purification
Tyre Shredding & Crumbing
Mechanical processing of scrap tyres to produce rubber shred, crumb rubber, and fine rubber powder while reclaiming steel wires.
Evaluated machinery, suppliers, and cost optimizations for rubber recycling projects at Rathi Rubber India and Modi Industries.
Mechanical sizing layout design, cutter/blade wear-life assessment, material classification consulting, and project feasibility review.
- Tyre Shredding Solutions
- Crumb Rubber Production
- Rubber Powder Generation
- Mechanical Classifier Setup
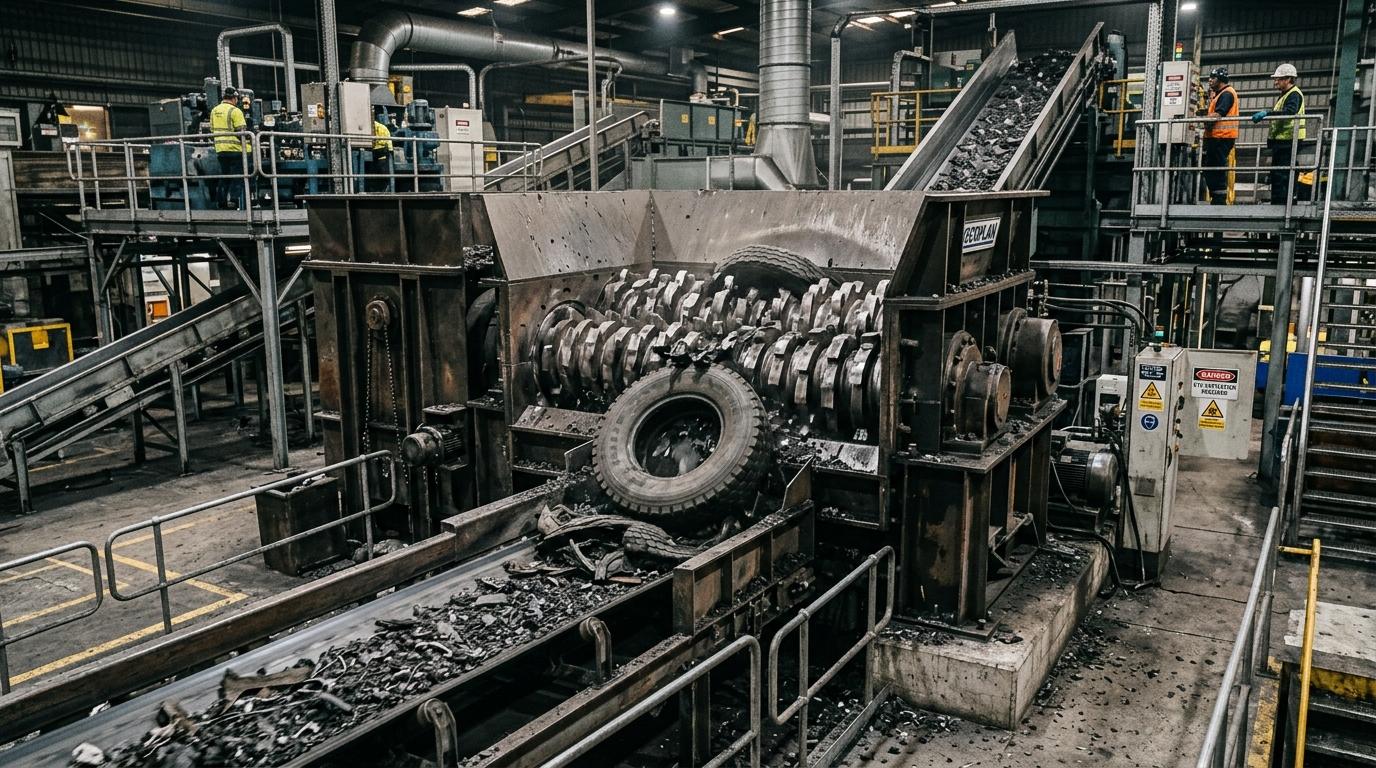
Mechanical Processing: Dual-shaft rotary shredder sizing tyres into crumb feedstock
Plastic & Biomass Pyrolysis
Thermochemical conversion of waste plastics and biomass feedstocks into synthetic fuels and solid bio-char products.
Advising chemicals and manufacturing groups on feedstock evaluation and alternative recycling technology viability since 2021.
Feedstock compatibility assessment, reactor technology risk review, and chemical process feasibility analysis.
- Plastic Waste Pyrolysis
- Biomass Thermochemical Conversion
- Feedstock Evaluation Metrics
- Pyrolysis Co-product Handling
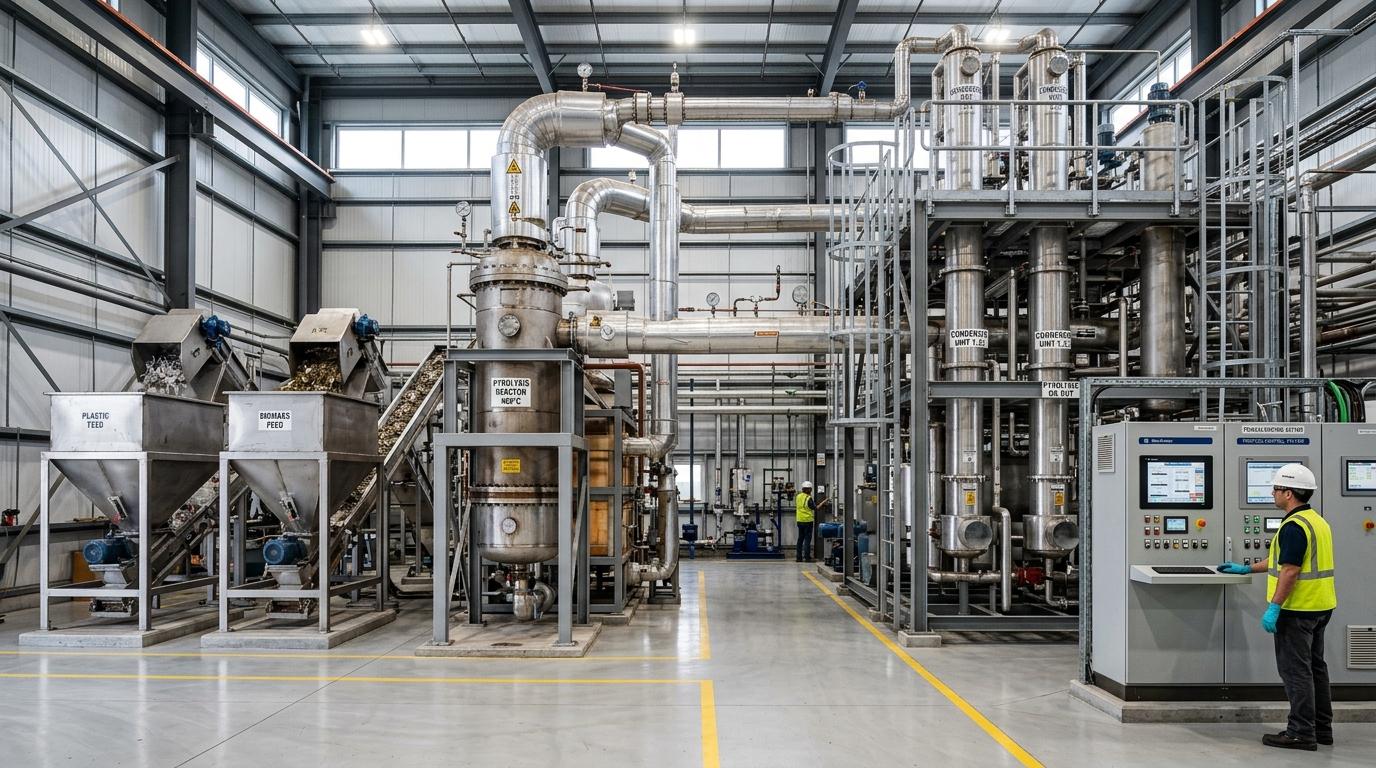
Alternative Feedstocks: Continuous thermochemical conversion unit with automated PLC monitoring
Base Oil Recovery
Refinery-grade recovery and reclamation of base oils from waste industrial lubricants and heavy petrochemical residues.
Operations and works management oversight across diverse chemical and API manufacturing sites (e.g. Vital Laboratories, Modi Industries).
Refinery and recycling consultation, quality compliance advisory, and value-added product optimization.
- Base Oil Recovery Processes
- Quality Compliance Advisory
- Reclamation System Design
- Value-added Product Optimization
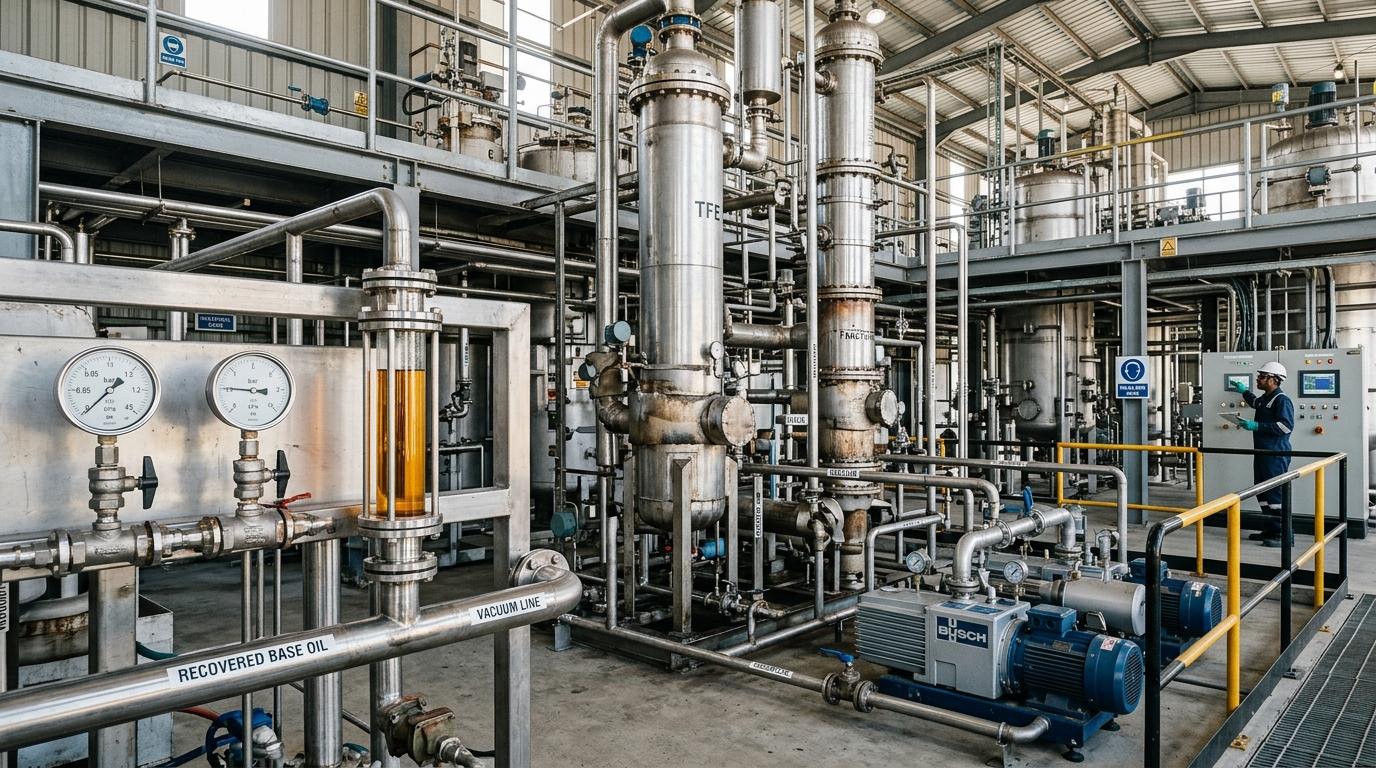
Refinery Reclamation: High-vacuum thin-film evaporator column with recovered oil sampling